Plastic injection moulding
From tooling toSerial production.
Technical thermoplastic components with DFM, tooling support, sampling and integrated finishing or assembly.
- 50–500 tClamping force
- UP TO 1,800 cm³Shot volume
- UP TO 2,500 g / SHOTDepending on material
- SINCE 1997Plastics manufacturing in Estonia
Injection moulding at Vesimentor
Technical components.Controlled from the start.
As a contract manufacturer, we produce injection-moulded plastic components for industrial customers, coordinating the decisions that affect the part, tool and production route before serial manufacturing begins.
DFM & material review
Geometry, service conditions and material requirements reviewed together.
Tooling & sampling
New tooling or existing tools assessed before serial release.
Serial production
Agreed process, quality criteria and documentation maintained for the project.
Finishing & assembly
Selected downstream operations included in one coordinated scope.
Design for moulding
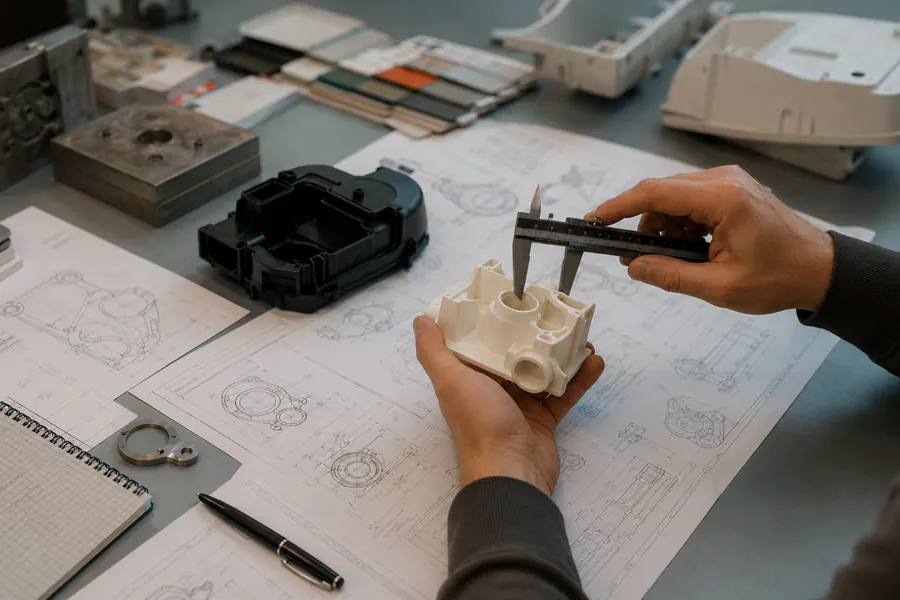
Make the part, tool andprocess work together.
Early DFM review helps align part function with a practical moulding route. Critical requirements should be visible in the drawing and agreed before tooling and sampling.
Wall thickness
Uniformity and transitions
Parting lines
Location and appearance
Draft angles
Release from the tool
Shrinkage & warpage
Material and geometry effects
Gates & ejection
Placement and witness marks
Surface & interfaces
Cosmetic and assembly areas
A controlled project route
From drawing toongoing supply.
- 01
Review
Part, function, annual quantity
- 02
Define
Material and critical requirements
- 03
Tool
New tool or tooling transfer
- 04
Sample
Process setup and approval
- 05
Produce
Controlled serial moulding
- 06
Complete
Finishing, assembly and delivery
Material selection
From part requirementsto the right grade.
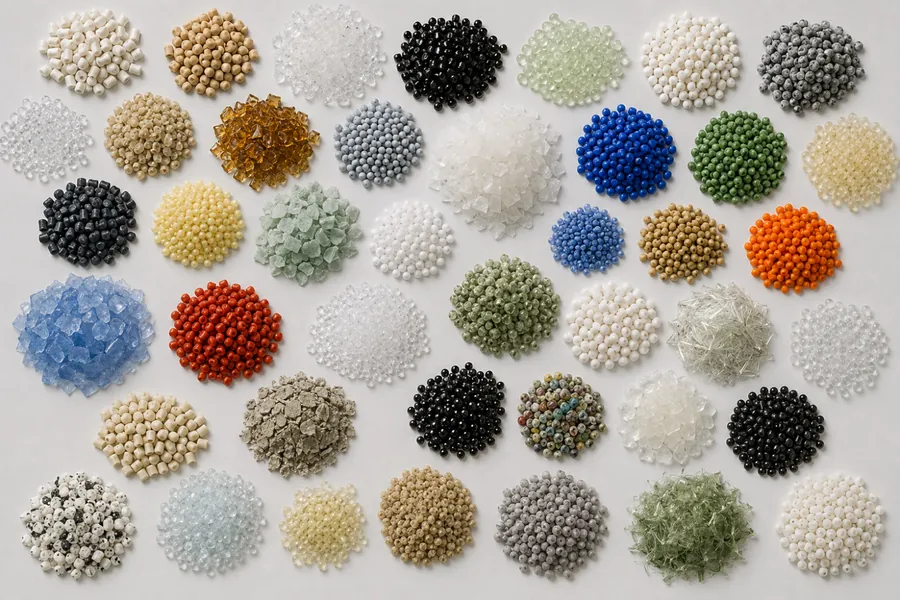
Material selection follows the mechanical, thermal, chemical, UV, cosmetic and regulatory requirements of the part, together with any downstream operations.
- PA
- PE
- PP
- ABS
- POM
- PC
- PC/ABS
- PMMA
Specific grades and suitability are reviewed project by project.
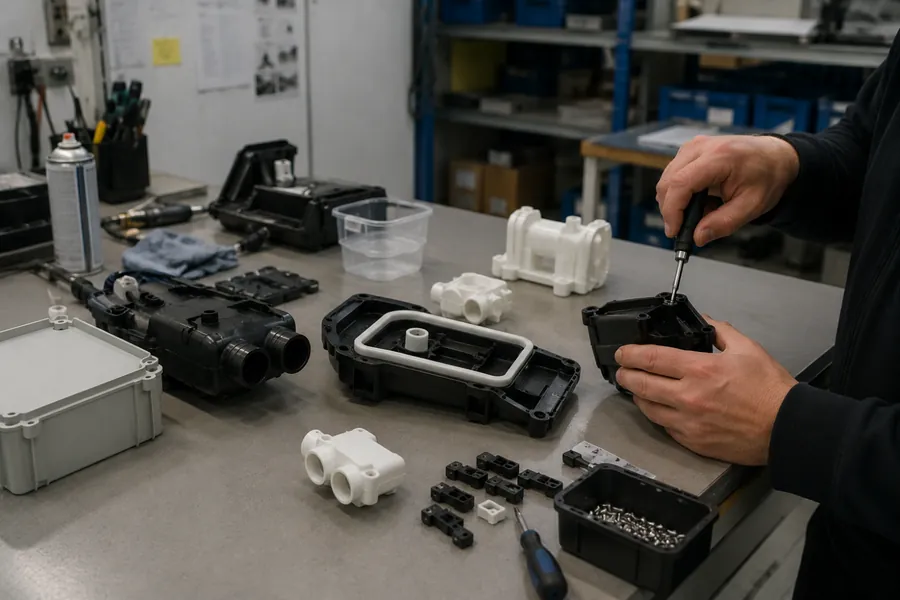
More than moulding
One part. One coordinated route.
Vacuum metallizing
Decorative or functional metal-effect finishes
FIPFG sealing & potting
Robot-dispensed foam gaskets and protection
CNC & ultrasonic welding
Post-processing and joining where required
Assembly & packaging
Components completed for the agreed delivery scope
Downstream operations are assessed together with the moulding route.
Combined-material components
Inserts & overmoulding.
Insert moulding
Specified inserts are incorporated into the plastic part during moulding. Insert geometry and retention features must be considered in the part and tool design.
EXPLORE INSERT MOULDINGOvermoulding
Plastic is moulded around an existing component or first-shot core. Material pairing, geometry and interface requirements determine suitability.
EXPLORE OVERMOULDINGSuitability is reviewed against the component, materials, tooling and available machine setup.
Typical applications
Contract injection mouldingfor technical plastic parts.
Vesimentor is a plastic injection moulding manufacturer in Pärnu, Estonia. Injection moulding is offered as a contract manufacturing service to industrial customers in the Baltic states, the Nordic countries and the rest of Europe.
Injection-moulded parts are supplied to the sanitary industry (toilet parts such as lids, internal components and floats, as well as mixer tap parts) and to electronics manufacturers.
Housings & enclosures
Moulded housings that can continue to FIPFG sealing and assembly.
Visible & reflective parts
Cosmetic surfaces and lighting components that can be vacuum metallized.
Parts with inserts or overmoulding
Metal inserts or a second material where the design requires it.
Small technical parts
Small components reviewed for geometry, material and critical dimensions.
Related pages: Overmoulding & insert moulding · Small technical parts · Metal-to-plastic conversion
These part types are typical for the process. Suitability of a specific design is confirmed in the project review.
New project or tool transfer
Start with the right information.
New component
Send a 3D model or dimensioned drawing, material requirements, annual quantity, critical dimensions, cosmetic surfaces and required finishing or assembly.
Existing tooling
Send the part data, tool information, current production status, expected volumes and any known quality or transfer requirements.
Up to 2,500 g per shot, depending on material. Shot weight is not a finished-part weight limit.
Injection mouldingQuestions
Vesimentor’s injection moulding machines cover 50–500 t clamping force, with shot volume up to 1,800 cm³ and shot weight up to 2,500 g per shot, depending on material. Final suitability depends on the component, material and tooling.
Material families include PA, PE, PP, ABS, POM, PC, PC/ABS and PMMA. The exact grade is reviewed against the mechanical, thermal, chemical, cosmetic, regulatory and downstream-process requirements of the project.
Yes. Existing tooling can be reviewed for transfer, condition, machine compatibility, part requirements and expected production volumes before the manufacturing route is agreed.
Yes. Depending on the project, the agreed scope may include vacuum metallizing, FIPFG sealing or potting, CNC post-processing, ultrasonic welding, assembly and packaging.
Yes. Injection molding is the American spelling of injection moulding. In both cases molten thermoplastic is injected into a closed mould, cooled and ejected as a finished part.
Yes. Vesimentor has manufactured plastic parts in Pärnu, Estonia, since 1997 and produces injection-moulded components to customer drawings. DFM review, tooling, sampling, serial production and any agreed finishing or assembly are planned as one project. Production operates under ISO 9001, ISO 14001 and AQAP 2110.
Have a part or project in mind?
Send us your drawings.
Share the 2D or 3D files, material requirements, expected volumes and required downstream operations. Our team will review the complete manufacturing route.